Lunasol Logistics
Choosing industrial automation is no longer a simple equipment decision. It affects safety, productivity, maintenance, data quality, and workforce capability. This article explores What Are The Best Practices For Industrial Automation in practical manufacturing environments.
Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 92% of surveyed manufacturers view smart manufacturing as a major competitiveness driver. However, many companies still struggle to scale pilot projects across entire plants. The gap often appears on the factory floor. A reliable system needs clear sensor data, tested PLC logic, visible safety interlocks, and maintenance teams who understand the equipment.
Automation industry analyst Jim Pinto described automation as “the technology by which a process or procedure is performed with minimal human assistance.” His definition highlights an important principle: automation should support controlled performance, not remove human judgment blindly. Effective practices include setting measurable goals, assessing process stability, protecting industrial networks, and planning for lifecycle maintenance. Standards from ISA and IEC also provide useful guidance for safety, cybersecurity, and system integration.
No checklist fits every plant. A packaging line may need faster changeovers, while a chemical process may prioritize containment and safety. Companies can also overinvest in dashboards before fixing inconsistent production data. That mistake deserves honest reflection. The strongest approach begins with a narrow, measurable use case, then expands after workers verify the results. This introduction will examine the decisions, standards, technologies, and human factors that make automation dependable rather than merely impressive.
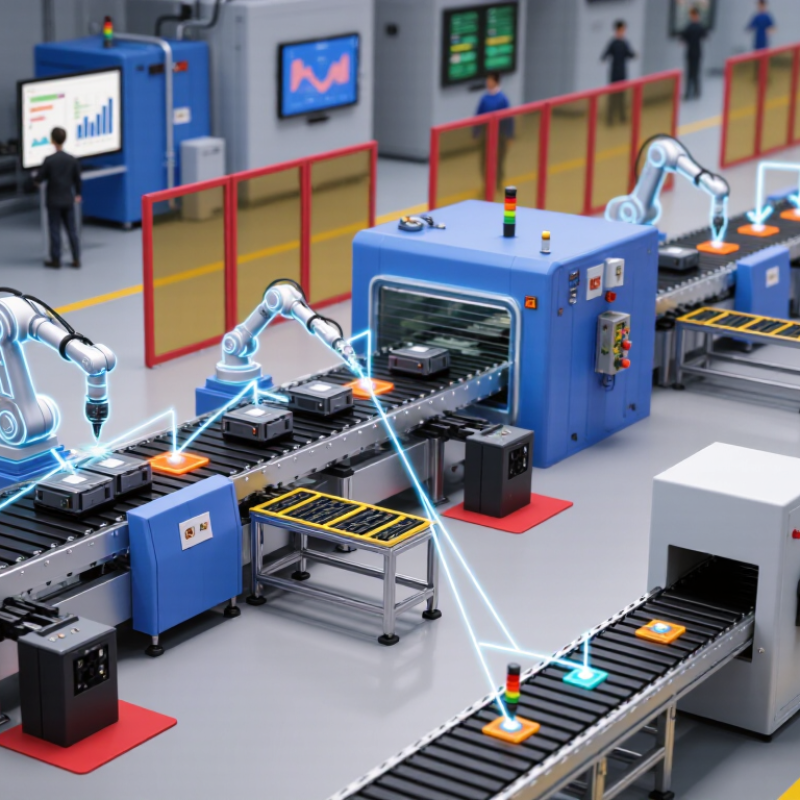
Define the project before choosing automation practices. Write down the business problem, not only the desired technology. Is the goal higher throughput, safer handling, fewer defects, or better traceability? The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. That growth does not prove automation will solve every factory problem. A clear baseline is essential. Record cycle time, unplanned downtime, scrap rates, labor hours, and energy use for several weeks. Set measurable targets, such as reducing changeover time by 20% within six months.
Scope must be equally specific. Identify the production line, processes, equipment, data sources, and responsible teams. Include maintenance and quality staff early. They understand practical constraints that planning meetings often miss. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders view smart manufacturing as important, yet many still struggle to scale initiatives. Ambition is common. Execution is harder.
Define what the first phase will not include. For example, automate one packaging cell before connecting the entire plant. Specify interfaces, safety requirements, training needs, cybersecurity controls, and acceptance tests. A useful scope document names every handoff, from sensor readings to operator actions. Leave room for revision. Our first assumptions may be wrong. A pilot can reveal unstable product demand, poor data quality, or inconvenient maintenance access. Treat these findings as evidence, not failure, and adjust the project before expanding it.
A practical planning matrix for translating business goals into measurable automation requirements, defined project boundaries, and implementation priorities.
| No. | Best Practice | Primary Goal | Recommended Project Scope | Measurable KPI and Typical Target | Required Evidence | Priority | Relevant Reference |
|---|---|---|---|---|---|---|---|
| 1 | Establish a documented business case | Align automation investment with operational, quality, safety, and workforce objectives. | Define the production line, process area, products, shifts, stakeholders, constraints, and expected benefits before selecting technology. | Approved benefit model covering at least cost, capacity, quality, safety, and delivery outcomes; financial assumptions reviewed by operations and finance. | Business-case document, stakeholder register, approved assumptions, and risk log. | High | Project governance practice |
| 2 | Create a current-state baseline | Prevent unrealistic targets by measuring actual process performance before automation. | Collect data from the selected process over representative products, shifts, operators, and operating conditions. | Baseline includes throughput, cycle time, downtime, changeover time, scrap, rework, labor hours, and energy use; measurement period normally covers multiple production cycles. | Time studies, production records, downtime logs, quality records, and energy measurements. | High | OEE measurement practice |
| 3 | Define SMART automation objectives | Convert broad intentions such as “increase efficiency” into testable project outcomes. | Set specific, measurable, achievable, relevant, and time-bound targets for each process segment included in the project. | Examples: reduce unplanned downtime by 10–20%; reduce manual data entry by 80%; improve first-pass yield by 3–5 percentage points; shorten changeover time by 15%. | Signed KPI tree, target definitions, calculation formulas, data owners, and acceptance thresholds. | High | Performance-management practice |
| 4 | Set clear scope boundaries | Control cost, schedule, and technical complexity by separating included work from excluded work. | Specify equipment, process steps, interfaces, utilities, software, data, training, commissioning, and support activities included in the initial release. | 100% of affected assets and interfaces have an owner; all exclusions have documented rationale, assumptions, and future-release treatment. | Scope statement, system boundary diagram, work-breakdown structure, interface list, and change-control process. | High | Systems-engineering practice |
| 5 | Prioritize the bottleneck process | Direct automation effort toward the constraint that limits total production output or delivery performance. | Analyze material flow, waiting time, machine availability, staffing, buffer levels, and downstream effects before selecting the first automation area. | Increase constraint throughput by a defined amount while avoiding the creation of a new downstream bottleneck; track throughput, queue time, and utilization. | Value-stream map, process-capacity model, bottleneck analysis, and before-and-after flow data. | High | Lean operations practice |
| 6 | Define safety requirements first | Ensure that automation improves productivity without introducing unacceptable risks to people, equipment, or facilities. | Cover operating modes, access points, emergency stops, safeguarding, maintenance access, restart behavior, foreseeable misuse, and safety-related control functions. | Risk assessment completed before detailed design; required safety functions validated before production release; residual risks formally accepted. | Risk assessment, safety requirements specification, safety circuit validation, lockout/tagout procedure, and training records. | High | ISO 12100; ISO 13849-1 |
| 7 | Define data and interoperability needs | Make operational data consistent, usable, secure, and available at the right decision level. | Specify data sources, tags, timestamps, naming conventions, quality states, retention, dashboards, reporting, and interfaces between control, supervisory, and business systems. | Critical data elements have defined owners, units, update rates, quality states, and retention periods; interface tests pass agreed acceptance criteria. | Data dictionary, tag list, network diagram, interface specification, sample reports, and integration test results. | High | ISA-95; IEC 62264 |
| 8 | Include cybersecurity in the initial scope | Protect industrial control systems from unauthorized access, disruption, and unsafe changes. | Assess zones and conduits, remote access, account management, backups, patching, malware protection, logging, incident response, and supplier access. | All critical assets inventoried; privileged access controlled; tested backups available; remote connections approved and monitored; high-risk findings assigned owners. | Asset inventory, network segmentation plan, access matrix, backup test record, vulnerability register, and incident-response procedure. | High | NIST SP 800-82; IEC 62443 |
| 9 | Design for maintainability and lifecycle support | Reduce long-term downtime and dependence on undocumented knowledge or unavailable parts. | Define diagnostics, spare parts, preventive maintenance, calibration, software version control, recovery procedures, obsolescence planning, and technical documentation. | Critical failure modes have detection and recovery procedures; maintenance tasks have defined intervals; backup and restore procedures are tested. | Maintenance plan, spare-parts list, alarm philosophy, recovery guide, software backups, and technician training records. | Medium | IEC 60300 lifecycle practice |
| 10 | Plan human factors and workforce adoption | Ensure operators, technicians, engineers, and supervisors can safely use and support the new system. | Include workstation design, HMI usability, role permissions, standard work, training, feedback channels, and transition arrangements for existing tasks. | Role-based training completed before go-live; critical tasks demonstrated successfully; user feedback actions closed before final acceptance. | Training matrix, standard operating procedures, usability review, competency checks, and adoption issue log. | High | Human-factors engineering practice |
| 11 | Use staged validation and acceptance gates | Detect design and integration problems before they affect production operations. | Define requirements review, design review, factory acceptance testing, site acceptance testing, commissioning, performance qualification, and operational handover. | Each gate has documented entry and exit criteria; all critical defects are closed or formally waived before production release. | Requirements traceability matrix, test protocols, defect log, acceptance records, and handover checklist. | High | Verification and validation practice |
| 12 | Define a controlled improvement roadmap | Deliver value in manageable stages while preserving future scalability and integration options. | Separate the minimum viable release from later enhancements such as advanced analytics, additional lines, predictive maintenance, or broader enterprise integration. | Roadmap includes release objectives, dependencies, budget ranges, decision gates, benefits review dates, and criteria for expanding or stopping the program. | Phased roadmap, benefits-realization review, architecture principles, investment gates, and lessons-learned register. | Medium | Continuous-improvement practice |
Start with a process map, not an equipment list. Record cycle times, stoppages, changeovers, defects, and manual handoffs. A faster machine may worsen a flawed process. That mistake is costly.
Compare observed delays with equipment capacity, safety controls, and maintenance access. Watch the line during normal and difficult shifts. A short pilot may expose hidden constraints. Do not trust assumptions alone.
Define measurements that support decisions, including temperature, torque, downtime, quality, and energy use. Check sensor accuracy, timestamps, ownership, and retention rules. Missing data creates false confidence. Dashboards cannot repair poor measurements.
Match the architecture to production needs. Local controllers suit discrete sequences and fast motion. Distributed systems suit continuous regulation and fault tolerance. Edge systems can filter equipment data nearby. Keep safety-critical commands local.
Request reference sites with similar loads, uptime targets, and working conditions. Review training, spare-part timing, documentation, firmware policies, and support coverage. Ask who owns configuration files later. A low price can hide integration work.
Walk the production floor before selecting equipment or control logic. Identify pinch points, heat sources, moving tools, and manual access areas. Emergency stops must remain visible and reachable. Test them regularly. Written procedures are not enough.
Maintain an accurate inventory of controllers, sensors, engineering stations, and remote connections. Separate critical networks from office systems. Use strong authentication and remove unused accounts. Keep offline backups of tested configurations. Small gaps matter.
Interview operators, technicians, supervisors, and maintenance teams before selecting technology. Train people on actual tasks, fault diagnosis, and safe recovery. Their practical knowledge may challenge the original design. Listen carefully.
Use consistent naming, documented interfaces, and modular control routines. Test new cells separately before connecting production systems. Verify timestamps, units, alarms, and data ownership. Operators should validate screens and workflows. Night shifts reveal weaknesses.
Treat failure as useful evidence, not immediate defeat. Record failed tests, delays, dust problems, and manual workarounds. Review the assumptions honestly before expanding. Perfect plans rarely survive real factory conditions.
What Are The Best Practices For Industrial Automation? The answer begins with clearly defining the project’s goals, scope, budget, timeline, and expected business outcomes. Organizations should carefully assess current processes, equipment, data flows, maintenance requirements, and workforce capabilities before selecting an automation strategy. This evaluation helps identify inefficiencies, operational risks, training needs, and opportunities for measurable improvement.
The next step is to compare suitable automation technologies, system architectures, and solution providers according to performance, compatibility, lifecycle cost, and support capabilities. Safety, cybersecurity, scalability, and integration with existing systems should be considered from the beginning rather than added later. A successful approach also includes a controlled pilot test, structured implementation plan, employee training, and performance monitoring. By reviewing results continuously and refining processes over time, companies can build a reliable, adaptable, and efficient industrial automation solution that supports long-term operational growth.